
What Is an Injection Moulding Machine Product?
Basic Definition: Plastic Injection Moulding Machine
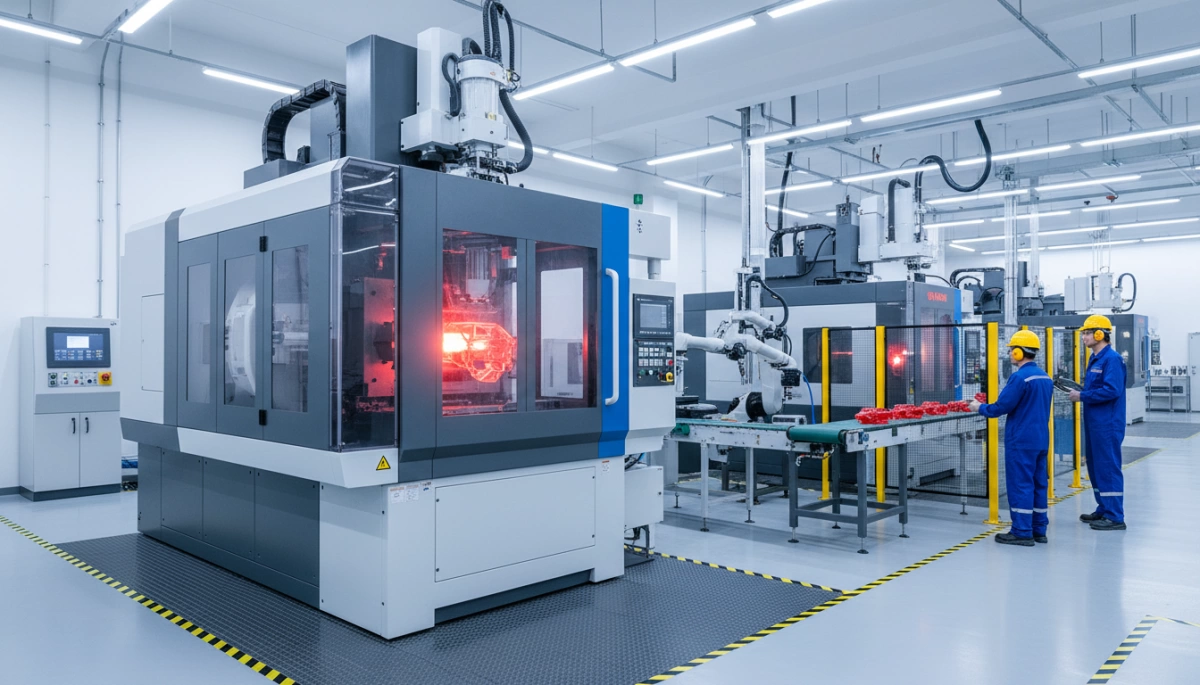
A plastic injection moulding machine (also called a plastic injection equipment or plastic part manufacturing machine) is an industrial machine that:
- Melts plastic pellets
- Injects the molten plastic into a mould
- Cools and ejects a finished plastic part automatically
In short, it’s a fully automatic system that turns raw plastic pellets into repeatable, high-volume plastic parts.
Core Function in Plastic Part Manufacturing
The main job of an injection moulding machine product is:
- Produce high volumes of identical parts
- Maintain tight tolerances and stable dimensions
- Run 24/7 with controlled cycle time and energy consumption
This is why injection moulding is the go-to choice for:
- Automotive trims, clips, and connectors
- Packaging caps, closures, and containers
- Medical, electronics, and consumer goods parts
Main Components of an Injection Moulding Machine Product
| Component | What It Does (Plain Talk) |
|---|---|
| Hopper | Holds and feeds plastic pellets into the machine |
| Barrel | Heats the plastic and keeps it at the right melt temperature |
| Screw | Rotates to melt, mix, and push plastic forward |
| Injection Unit | Measures (shot size) and injects molten plastic into the mould |
| Clamping Unit | Opens/closes the mould and provides clamping force (tonnage) |
| Tie Bars & Platens | Support the mould and keep it aligned under pressure |
| Controller | The “brain” – sets temperature, pressure, speed, cycle, and alarms |
These core components define the performance and reliability of any industrial injection moulding machine.
How the Injection Moulding Process Works
Here’s the step‑by‑step injection moulding process in simple terms:
- Feeding
Plastic pellets drop from the hopper into the barrel. - Melting & Mixing
Heaters and the screw melt the pellets into a uniform melt. - Metering (Shot Build-Up)
The screw moves back and prepares a defined shot size (the volume for one part or set of parts). - Injection
The clamping unit closes the mould.
The screw moves forward, injecting plastic at controlled injection pressure into the cavity. - Packing & Holding
Extra pressure compensates for shrinkage and keeps the cavity packed for good surface and dimensions. - Cooling
The part cools inside the mould with built‑in cooling channels. - Mould Opening & Ejection
The clamp opens, ejector pins push the part out, and the cycle repeats.
This automatic injection moulding process is what gives you high output and consistent quality.
How Injection Moulding Machines Differ from Other Plastic Processing Equipment
Not all plastic machines do the same job. Here’s how an injection moulding machine product compares:
| Equipment Type | Main Use | Key Difference vs Injection Moulding Machine |
|---|---|---|
| Injection Moulding Machine | Complex 3D parts with high volume | Uses a mould and clamping force for precision |
| Extrusion Line | Continuous profiles, pipes, films | No mould cavities; continuous product, no cycles |
| Blow Moulding Machine | Hollow parts (bottles, tanks) | Uses air to blow plastic into shape |
| Thermoforming Machine | Trays, thin sheets shaped by heat and vacuum | Starts from sheet, not pellets and screw process |
| Rotational Moulding Machine | Large hollow parts (tanks, kayaks) | Slow cycles, powdered resin, rotating moulds |
If you need repeatable, dimensionally accurate plastic parts with tight tolerances and fast cycle times, a plastic injection moulding machine product is almost always the right choice.
Injection Moulding Machine Product Types
When you choose an injection moulding machine product, the type of drive, layout, and tonnage will decide your part quality, speed, and running cost. Here’s how I look at it in real projects.
Hydraulic Injection Moulding Machine Products
Hydraulic injection moulding machines are tough, proven, and forgiving on rough factory conditions.
Best fit:
- Thick‑wall parts, automotive components, pallets, crates
- Jobs where high clamping force and ruggedness matter more than ultra‑low energy use
- Plants with operators already familiar with hydraulic systems
Key points:
- Strong and reliable for large tonnage injection moulding machine needs
- Easier to service in many regions due to common hydraulic parts
- Slightly higher energy consumption vs all‑electric, but cheaper upfront
All Electric Injection Moulding Machine Products
An all electric injection molding machine is about precision, clean operation, and energy savings.
Best fit:
- Medical plastic injection equipment, consumer electronics, precision connectors
- Cleanroom or low‑noise environments
- High‑cavitation molds where shot‑to‑shot repeatability is critical
Key points:
- High accuracy on position, pressure, and speed
- Strong energy efficient molding machine performance, lower running cost
- Higher initial price but better long‑term ROI for high-volume production
Hybrid Injection Moulding Machine Products
A hybrid injection molding machine combines electric drives with hydraulic power where it makes sense.
Best fit:
- Automotive, packaging, and technical parts that need both speed and force
- Users wanting a balance between hydraulic injection molding machine robustness and electric efficiency
Key points:
- Electric servo for injection/plasticizing, hydraulic for clamp or core pulls
- Good mix of speed, power, and energy saving
- Flexible option when you run many different molds and materials
Horizontal vs Vertical Injection Moulding Machine Products
Horizontal injection moulding machines:
- Standard choice for most plastic part manufacturing machines
- Fast cycling and easy to automate with robots and conveyors
- Ideal for high-volume, fully automatic production lines
Vertical injection moulding machines:
- Great for overmolding injection machine applications with inserts, metal parts, or cables
- Space-saving design in some setups
- Easier manual or semi-automatic loading of inserts
Small Tonnage vs Large Tonnage Injection Moulding Machines
Choosing between a small injection moulding machine and a large tonnage injection moulding machine is mainly about part size and mold area.
- Small tonnage (e.g. 30–200T)
- Precision parts, electronics, caps, medical disposables
- Faster cycles, less energy, smaller footprint
- Medium to large tonnage (e.g. 250–2000T+)
- Automotive bumpers, bins, crates, furniture, appliance housings
- Handles bigger molds and higher clamp forces without flash
If you want a quick feel for how different machine types work and where each fits in a production line, I walk through typical setups on our injection moulding machine product overview page, including hydraulic, electric, and hybrid options.
Key Specifications of an Injection Moulding Machine Product
When I spec an injection moulding machine product, I focus on a few core numbers. These decide if the machine will actually run your parts smoothly and profitably.
Clamping Force (Tonnage)
Clamping force keeps the mold shut against injection pressure.
| Spec | What it Means | Simple Rule of Thumb |
|---|---|---|
| Clamping force | Pressing force on the mold (kN / tonnage) | Match to part projected area × cavity count |
| Typical range | 30T – 3000T+ | Small parts: 30–200T / Auto parts: 500T+ |
- If tonnage is too low → flash, unstable molding.
- If tonnage is too high → wasted cost, higher energy use.
- For basics on parts vs mold design, see this guide on plastic injection moulding products.
Injection Unit Specifications
These define how much material you can inject, and how precisely.
| Spec | Description | Why it Matters |
|---|---|---|
| Shot size | Max plastic per shot (cm³ / g) | Must cover part + runner + safety margin |
| Injection pressure | Force pushing melt into the cavity | Needed for thin walls / complex geometry |
| Screw diameter | Size of plasticizing screw | Impacts plasticizing rate & shot stability |
| L/D ratio | Screw length/diameter ratio | Affects mixing, melt quality, color changeover |
- Always calculate shot size from your heaviest part (including runner, sprue, cold slug).
Tie Bar Spacing, Platen Size, Mold Dimensions
The mold must physically fit the plastic injection equipment.
| Spec | Role |
|---|---|
| Tie bar spacing | Max mold width/height between tie bars |
| Platen size | Mounting surface for the mold |
| Mold height range | Min/Max mold thickness machine can accept |
| Daylight | Max open distance (for ejection & robot) |
- A common mistake: tonnage is OK, but mold doesn’t fit between tie bars.
Cycle Time and Dry Cycle Speed
These numbers drive your output and part cost.
| Spec | Meaning |
|---|---|
| Cycle time | Full molding cycle (sec) |
| Dry cycle speed | Open/close speed without load |
- Faster dry cycle + optimized cooling = lower part cost.
- For high-volume jobs, even 1–2 seconds saved per cycle has a big impact.
Energy Consumption & Drive System
Energy is a big part of lifetime cost for industrial injection moulding machines.
| System Type | Key Benefit |
|---|---|
| Hydraulic injection moulding | Strong, robust, lower initial cost |
| Servo hydraulic | Lower power use vs standard hydraulic |
| All electric injection | High precision, best energy efficiency |
- Look at kWh/kg or kWh/shot, not just motor size.
- Energy efficient molding machines pay off fast on 24/7 production.
Control System & Automation
Modern control systems turn a machine into a stable plastic molding production line.
Key functions I always insist on:
- Closed-loop control for pressure, speed, and temperature
- Recipe storage for different molds / materials
- Real-time monitoring: alarms, trends, basic data tracking
- Connectivity for Industry 4.0 / MES (Ethernet, OPC UA, etc.)
This lets you run more consistent cycles and support data-driven production.
Optional Configurations and Specials
Depending on your product line, the right options can save you tools, labor, and scrap:
- Hot runner systems – Less waste, faster cycles, better gate control
- Multi-shot / double-shot injection moulding – Two materials or colors in one cycle (see how we use it in our double-shots injection moulding setups)
- Overmolding injection machine – Hard + soft material, inserts, metal cores
- Gas assist – Thick parts with lower weight and less sink marks
- Core-pull, unscrewing, inserts – For threads, undercuts, and complex shapes
When you choose a plastic injection moulding machine, always tie these specifications back to your real parts, volumes, and long-term running cost—not just the headline tonnage.
Core Features Buyers Look For in Injection Moulding Machine Products
When I choose or recommend an injection moulding machine product, I always focus on a few core features that really decide part quality, running cost, and long‑term ROI.
1. Precision & Repeatability
A plastic injection moulding machine lives or dies on consistency.
What matters:
- Stable injection pressure and speed
- High‑resolution control of screw position and back pressure
- Rigid clamping to keep the mould aligned
- Accurate temperature control on barrel and mould
Why it matters:
You get tight tolerances, less scrap, and reliable quality on repeat orders – critical for automotive, medical, and consumer electronics parts.
2. Energy Efficiency & Running Cost
Energy is one of the biggest ongoing costs in plastic part manufacturing.
Key points buyers look at:
- Servo‑hydraulic or all electric injection molding machine drives
- Optimized cycle time and dry cycle speed
- Intelligent standby and power‑saving modes
- Verified kWh per kg of plastic processed
Well‑specified energy efficient molding machines can cut total lifecycle cost more than a cheap machine ever could.
3. Stability, Rigidity & Durability
The frame and platen system of an industrial injection moulding machine must stay rigid under high clamping force.
Core structural features:
- Heavy‑duty frame with low deflection
- Robust tie bars and platens
- Long‑life screw, barrel, and bearings
- Corrosion‑resistant and wear‑resistant materials
This is what keeps parting lines tight, reduces flash, and extends machine life.
4. User‑Friendly Control System
Modern automatic injection moulding machines need smart but simple controls.
What I expect:
- Intuitive touchscreen HMI
- Clear setting pages for temperature, pressure, speed, timing
- Recipe storage for mold and material setups
- Real‑time trend graphs and alarms
- Data logging for process monitoring and traceability
A good injection machine control system makes it easier to dial in stable processes and support Industry 4.0 integration.
5. Safety & Compliance
Safety is non‑negotiable with high‑pressure plastic injection equipment.
Core safety features:
- Dual safety gates and interlocks
- Light curtains or area scanners on large tonnage injection moulding machines
- Emergency stop circuits with category‑rated components
- Compliance with CE, ISO, or local safety standards
You protect operators and avoid costly downtime and legal issues.
6. Automation & Integration
Most buyers now plan a full plastic molding production line, not just a stand‑alone machine.
Integration must‑haves:
- Standard interfaces for robots, pick‑and‑place, and IML systems
- I/O and communication for conveyors, mold temperature controllers, and dryers
- OPC UA / Euromap or similar protocol for Industry 4.0 injection moulding machine connectivity
This is how you build a stable, automated cell that can run high‑volume jobs profitably.
Quick Comparison Table
| Feature | Why Buyers Care | What a Good Machine Offers |
|---|---|---|
| Precision & repeatability | Dimensional accuracy, low scrap | Servo control, rigid clamp, stable melt temperature |
| Energy efficiency | Lower kWh cost, greener production | Servo drive injection machine or all-electric |
| Frame stability & durability | Long life, minimal flash, less downtime | Heavy frame, strong platens, quality materials |
| User-friendly control system | Faster setup, fewer mistakes | Touchscreen HMI, recipes, data logging |
| Safety & standards compliance | Operator safety, legal compliance | Interlocks, guards, CE/ISO compliance |
| Automation integration | Higher output, lower labor costs | Robot interfaces, conveyor and peripheral links |
If you’re sizing a machine and planning tooling at the same time, it’s worth checking detailed guides on both injection mould tooling and full injection moulding price breakdowns so your machine choice, mold design, and cost targets line up from day one.
Applications of Injection Moulding Machine Products
Our injection moulding machine products are built to cover almost every plastic application you see in the global market today. Here’s where they make the most impact.
Automotive Plastic Components
For automotive plastic injection moulding, stability and repeatability are critical. We use servo hydraulic and all electric injection molding machines to produce:
- Interior trims, clips, brackets, connectors
- Under-the-hood parts that must handle heat and vibration
- Functional components like fan housings and fluid tanks
Consistent clamping force and tight injection unit specifications keep parts in spec even on long production runs.
Packaging: Caps, Closures & Thin-Wall
In packaging, speed is money. Our plastic injection moulding machines are tuned for:
- Caps and closures
- Food containers and tubs
- Thin-wall packaging that needs ultra-fast cycles
With high-speed horizontal injection moulding machines, optimized cycle time, and energy-efficient servo drives, we help packaging plants hit volume targets and cut cost per part.
Medical & Healthcare Plastics
Medical customers need clean, stable and traceable production. For medical plastic injection equipment, we focus on:
- Disposables (syringes, tips, housings)
- Device components and connectors
- Precision parts for diagnostic equipment
Our machines work well with validated tooling and can be paired with cleanroom setups, process monitoring, and data logging. For high-precision medical work, we often recommend our all electric injection molding machine setups or tightly controlled servo drive injection machines.
If you’re looking to outsource production, our precision plastic injection moulding services are already geared for medical, electronics, and industrial parts.
Consumer Electronics & Precision Parts
For consumer electronics housings and small precision parts, dimensional accuracy and surface finish are everything. Our automatic injection moulding machines are widely used for:
- Phone and tablet housings
- Remote controls, chargers, connectors
- Small gears and technical components
Here we leverage hybrid injection molding machines and multi-cavity tools to balance speed, precision and cost.
Household Goods, Toys & Daily-Use Plastics
Our industrial injection moulding machines also run high-volume consumer parts:
- Storage boxes, kitchenware, household organizers
- Toys and educational products
- Everyday items like handles, knobs, clips
Customers in this segment often start with a small injection moulding machine and scale up as demand grows, so we design machines that are easy to run and maintain, even for lean teams.
Custom & Niche Plastic Parts
For niche industries, we support custom plastic part manufacturing using:
- Multi shot injection moulding machines for 2K/3K parts
- Overmolding injection machines for metal inserts, soft-touch grips
- Special materials (engineering plastics, recycled materials, additives)
We work closely with customers to match clamping force tonnage, shot size, and moulding machine energy consumption to the real production need, not just the catalog spec.
If you need both tooling and production support, our plastic injection mould manufacturer and factory capabilities can take you from idea to mass production with a single team.
How to Match an Injection Moulding Machine Product to Your Project
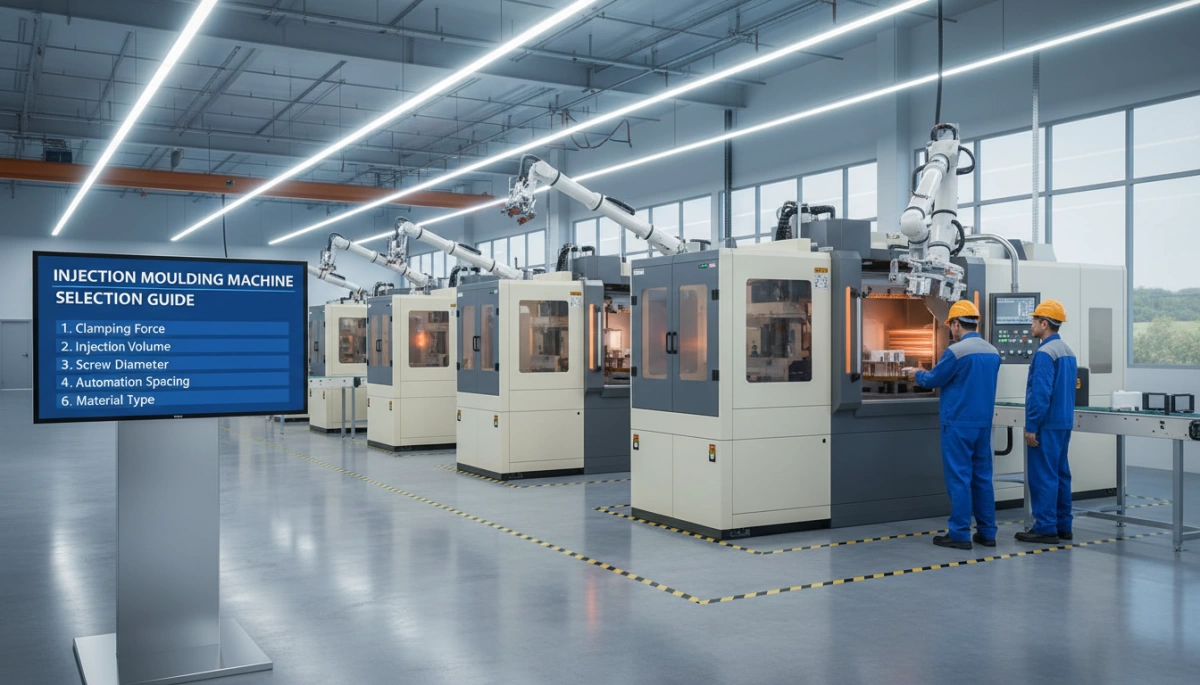
You don’t start with the machine; you start with the part. Once the part is clear, the “right” plastic injection moulding machine becomes obvious.
1. Lock in part size, weight & geometry
First, define the plastic part clearly:
| What you define | Why it matters for the machine |
|---|---|
| Max length, width, height | Sets platen size, tie-bar spacing, mold size |
| Part weight (in grams) | Drives shot size selection and screw diameter |
| Wall thickness & ribs | Affects injection pressure and material flow requirements |
| Number of cavities | Impacts clamping force and shot size |
Tip: Total shot volume (part + runner) should usually be 30–80% of the machine’s max shot capacity for stable molding.
2. Estimate volume & target cycle time
Your production plan decides how “big” and how “fast” the machine must be:
| Project type | Typical need |
|---|---|
| Prototyping / low volume | Small injection moulding machine, flexible setup |
| Mid-volume batches | Stable, mid-tonnage automatic injection moulding machine |
| High-volume mass production | High-speed, energy-efficient molding machines |
Define:
- Annual volume (pcs/year)
- Cycle time target (sec/shot)
- Required OEE (overall efficiency)
Then back-calculate how many cavities and what machine speed you really need.
3. Pick clamping force & shot size correctly
Clamping force (tonnage):
Basic rule of thumb:
Tonnage (ton) ≈ Projected part area (cm²) × Cavity count × 0.35–0.5
- Thin-wall packaging / high pressure → use higher factor
- Simple, thick-wall parts → lower factor often works
Shot size:
- Total shot (part + runner) = 30–80% of machine’s max shot
- For precision parts, stay closer to 30–60% for better process control
If you want the deeper math for how the injection molding process steps affect filling and pressure, this breakdown of how plastic injection moulding works is a solid reference when you spec the machine.
4. Match plastic material & melt characteristics
Not every plastic injection equipment handles every resin equally well. Check:
- Material type: PP, PE, ABS, PC, PA, POM, TPU, etc.
- Melt temperature range → heater and barrel design
- Viscosity / flow index → screw design, injection pressure
- Fiber filled / reinforced → stronger screw, wear-resistant barrel
- Use of recycled material → stable plasticizing, good mixing
For demanding materials, I usually match a specific screw design (L/D and compression ratio) and a stable temperature control system.
5. Check floor space, power & cooling
Before you sign for a plastic injection moulding machine, confirm your plant can support it:
| Factor | What to check |
|---|---|
| Floor space | Machine footprint + mold change + robot/conveyor area |
| Power supply | Voltage, phase, available kW vs machine demand |
| Cooling system | Chiller capacity, cooling water flow & temperature |
| Air supply | Compressor size for valves, core pulls, air blast |
Horizontal injection moulding machines usually need more length; vertical injection moulding machines need more height but less footprint.
6. Balance budget, performance & scalability
You’re not just buying an injection molding machine product for today; you’re buying it for the next 8–12 years.
Key trade-offs:
- Hydraulic vs all electric vs hybrid
- Hydraulic: lower upfront cost, strong for general parts
- All electric: higher precision, lower energy consumption
- Hybrid / servo hydraulic: good balance of power and efficiency
- Now vs future needs
- Slightly oversizing tonnage & shot can let you grow with new molds
- Choosing a machine with automation-ready interfaces (robots, conveyors, MES) makes upgrades cheaper later
- Total cost, not just price
- Energy use
- Maintenance and parts
- Downtime risk
- Operator time
If you’re planning molds with hot runners, multi-cavity or advanced injection molding machine types (like overmolding or multi-shot), make sure the control system and hydraulic/servo circuits are prepared from day one.
When I spec a plastic molding production line for global customers, I always run a quick ROI sheet: machine price + tooling + utilities vs output, scrap rate, and labor. That’s the only way to see which injection moulding machine product truly fits your project, not just your budget this month.
Buying Guide for Injection Moulding Machine Products
Choosing the right injection moulding machine product is a long-term decision. Here’s how I would break it down if I were buying for my own plant.
New vs Used Injection Moulding Machines
New machines – Pros:
- Latest technology (servo, all-electric, Industry 4.0-ready)
- Lower energy consumption and better process control
- Full warranty, training, and OEM service support
New machines – Cons:
- Higher upfront price
- Longer lead time in some regions
Used machines – Pros:
- Much lower capital cost
- Faster delivery and startup
- Good option to test a new project or niche product
Used machines – Cons:
- Higher risk of wear (screw/barrel, pumps, valves)
- May be less energy efficient
- Limited or no warranty; harder to get spares
If you’re looking specifically at used injection moulding machine for sale, I always recommend going through a specialist reseller that can provide inspection, test reports, and support. For example, a platform like the used injection moulding equipment section at Jino Plastics is designed exactly for that.
Key Questions to Ask Your Supplier
Before you buy any plastic injection moulding machine, ask:
- What is the real shot size and usable clamping force for my mold?
- What materials has this machine previously processed (for used)?
- What’s included: training, installation, starter spare parts, oil, warranty terms?
- Can you show energy consumption data for my cycle and material?
- How fast can you provide critical spare parts and service?
- Can I see the machine running my mold or a similar mold?
How to Compare Quotes and Technical Offers
When comparing injection moulding machine products from different brands, don’t just look at price:
- Specs: clamping force, shot size, injection speed, tie bar spacing, platen size
- Drive type: hydraulic, servo-hydraulic, all electric, hybrid
- Control system: screen size, data logging, remote support, integration options
- Energy use: kWh per kg of plastic or per cycle
- Service network: local engineer availability and response time
Create a simple comparison table and normalize everything to your part weight, material, and target cycle time.
Hidden Costs to Watch
These often hit buyers after the PO:
- Tooling (mould cost) – usually the biggest single cost
- Cooling system: chiller, cooling tower, piping
- Compressed air: compressor size and air treatment
- Accessories: dryer, loader, mixer, granulator, robot, conveyors
- Maintenance: hydraulic oil, filters, heaters, seals, spare screw/barrel
- Installation: rigging, electrical work, foundations, safety fencing
Always ask for a full system quote, not just the injection moulding machine price.
How to Test an Injection Moulding Machine
Before committing, you want to see real plastic parts:
- Run your own mold if possible, otherwise a mold close in size and material
- Check start-up time, cycle time, and repeatability over at least 1–2 hours
- Measure part weight variation across multiple shots
- Look for defects: short shots, burn marks, flash, sinks, warpage
- Monitor pressure and speed stability in the controller trend graphs
If you are buying used, insist on a live trial or a video of the machine running, ideally with documented parameters. A curated source like Jino’s used injection moulding equipment listings usually provides this type of transparency.
Calculating Long-Term ROI and Payback
To judge if an industrial injection moulding machine is worth it, run basic numbers:
- Total investment
- Machine + auxiliaries + mold(s) + installation
- Operating cost per hour
- Energy + labor + material loss + maintenance
- Parts produced per hour
- Cavitation × 3600 / cycle time (seconds)
- Cost per part
- Operating cost per hour ÷ parts per hour
- Profit per part
- Selling price – total cost per part (including amortized tooling)
- Payback period
- Total investment ÷ annual net profit from that machine
Often, a more expensive energy efficient molding machine (servo or all electric) pays back faster due to lower power bills and higher uptime. Always think in terms of lifetime cost, not just machine price.
Top Brands and Market Trends in Injection Moulding Machine Products
Global Injection Moulding Machine Manufacturers
The plastic injection moulding machine market is dominated by a few strong players that set the pace on technology and reliability. Names like Engel, Arburg, KraussMaffei, Sumitomo (SHI) Demag, Husky, Haitian, Milacron, and Nissei are well known for industrial injection moulding machines that cover everything from small precision parts to large automotive panels. These brands compete heavily on servo-hydraulic systems, all-electric technology, energy-efficient molding machines, and integrated automation to reduce cycle time and total cost per part.
Positioning of JINO Injection Moulding in the Market
JINO injection moulding sits in the value-focused segment: solid performance, competitive pricing, and strong support for global customers who need reliable plastic injection equipment without paying “premium European” pricing. We focus on servo hydraulic injection machines and energy efficient molding machines that deliver stable clamping force, consistent shot size, and smart controls. For buyers who also need a stable injection moulding manufacturer in China, we position JINO as a one-stop partner for both machines and plastic molding production line support, including mold optimization and material selection.
Shift to All-Electric and Servo-Driven Machines
Across all regions, demand is moving from basic hydraulic injection molding machines to servo drive injection machines and all electric injection molding machines. The key reasons are:
- Lower energy consumption and reduced heat build-up
- Higher precision and repeatability for thin-wall and medical parts
- Faster response on injection speed and hold pressure
- Cleaner operation, ideal for medical plastic injection equipment and electronics
Hybrid injection molding machines that combine hydraulic power with servo-electric drives are also growing, especially where high tonnage and high precision are both needed.
Industry 4.0, Smart Monitoring, and Data-Driven Production
Modern plastic injection moulding machines are quickly becoming connected assets. Buyers now expect:
- Real-time monitoring of cycle time, injection pressure, and energy consumption
- Automatic data logging for traceability and process validation
- Remote diagnostics and software updates
- Integration with MES/ERP for full production visibility
Our injection machine control system is designed for Industry 4.0, making it easier to track part quality, optimize process windows, and manage multiple machines as one connected plastic molding production line.
Sustainability and Energy Reduction
Sustainability is now a core buying driver for every injection moulding machine product:
- Recycled materials: Machines must handle regrind and recycled polymers with stable plastification. Pairing the right machine with the right injection moulding material is critical to keep quality high when using recyclate.
- Lower energy use: Servo hydraulic and all-electric machines can cut energy usage by 30–60% compared with older hydraulics.
- Reduced scrap: More precise control of temperature, injection speed, and pressure directly cuts scrap rate and improves ROI.
Brands that prove clear savings in kWh per kg of plastic and lower scrap rates are winning more projects.
Regional Differences in Injection Moulding Machine Demand
Demand for injection moulding machine products looks different by region:
- Europe & Japan: Strong preference for all electric injection molding machines, high automation, and full Industry 4.0 integration. Focus on medical, high-end packaging, and precision technical parts.
- North America: Mix of large tonnage injection moulding machines for automotive and logistics, plus mid-size presses for packaging and consumer goods. Strong interest in hybrid and servo-hydraulic machines for balanced cost and performance.
- China & wider Asia: Very dynamic market, with high volume demand for cost-effective automatic injection moulding machines, plus rapid growth in servo drive injection machines and Industry 4.0-ready systems as factories upgrade.
- Emerging markets (Southeast Asia, Latin America, Africa): Fast-growing need for robust, easy-to-maintain plastic injection moulding machines with lower initial investment and simple operation, but rising expectations for energy efficiency and reliability.
As an equipment provider, I design and position our injection moulding machine products to fit these regional needs: competitive pricing, stable quality, energy efficiency, and smart features that actually matter on the shop floor.
Maintenance for Injection Moulding Machine Products
Keeping an injection moulding machine product in top condition is non‑negotiable if you care about part quality, uptime, and energy costs. Whether you’re running a small injection moulding machine or a full plastic molding production line, a clear maintenance routine will pay for itself fast.
Daily, Weekly, and Monthly Maintenance Checklists
I always break maintenance down into simple, repeatable checklists:
Daily checks:
- Check oil level, temperature, and any leakage around the hydraulic system
- Inspect nozzle, screw tip area, and mold interface for material build‑up
- Verify safety doors, light curtains, and interlocks are working
- Listen for unusual vibration or noise from pumps, motors, or the screw drive
Weekly checks:
- Inspect tie bars, nuts, and platens for cracks, rust, or misalignment
- Check hose connections, heaters, and thermocouples for damage
- Test clamping force consistency and basic injection pressure stability
Monthly checks:
- Check alignment of the injection unit and clamping unit
- Inspect electrical cabinet: loose terminals, dust, fan filters
- Review alarms and production data from the control system to spot trends
Cleaning, Lubrication, and Screw/Barrel Care
Clean machines run more stable cycles and give you fewer moulding defects.
- Cleaning: Regularly clean the hopper, throat, and area around the barrel and nozzle to prevent contamination and black specks.
- Lubrication: Follow the lubrication chart for guide rails, toggle joints, and moving platens. Use the recommended grease/oil, don’t mix types.
- Screw & barrel care:
- Purge when changing material or color
- Avoid running at extreme back pressure or overspeed
- Don’t let material sit and bake at high temperature during long stops
Proper screw/barrel care directly cuts down on issues like burn marks and black spots, as discussed in many troubleshooting guides on controlling flash and other injection moulding defects.
Hydraulic Oil Management and Filter Replacement
On hydraulic and servo hydraulic injection machines, oil is the “blood” of your system.
- Use the correct oil grade and keep it within the recommended temperature range
- Monitor oil cleanliness with filters and particle indicators if available
- Change filters as per schedule or sooner if you see pressure drops or contamination alarms
- Replace oil when it darkens, smells burnt, or lab tests show high contamination
Good oil management extends pump life and keeps your hydraulic injection moulding machine stable.
Calibrating Sensors, Heaters, and Control Systems
For an automatic injection moulding machine, control accuracy is everything.
- Temperature sensors & heaters: Check barrel, nozzle, and mold temperature readings vs an external thermometer; recalibrate if there’s drift
- Pressure and position sensors: Calibrate injection pressure, back pressure, and screw position sensors regularly
- Control system:
- Back up parameters and recipes
- Update firmware/software as recommended
- Verify safety and alarm logic after any service
Accurate calibration is key to repeatable process windows and consistent shot size.
Preventive Maintenance to Reduce Downtime
Preventive maintenance is far cheaper than emergency repairs.
- Schedule PM stops based on running hours, not just calendar dates
- Combine PM with mold changes or planned line shutdowns
- Track common faults, energy consumption, and cycle consistency to see early warning signs
- Use Industry 4.0 / data tracking functions on modern injection moulding machine products to plan service instead of reacting to breakdowns
Signs You Need Repair, Overhaul, or Upgrades
Don’t wait until the machine fails on a key order.
You probably need repair or an overhaul if you see:
- Increasing scrap: flash, short shots, burn marks, warpage tied to machine inconsistency
- Big drift in injection pressure, shot weight, or cushion despite same settings
- Slow response from pump, lagging clamp movement, or unstable cycle time
- Frequent alarms on temperature, pressure, or safety circuits
You should consider an upgrade when:
- Energy consumption is too high vs modern energy efficient molding machines
- Cycle times can’t meet current market demands
- You want better automation, monitoring, or integration with robots
A well‑maintained plastic injection moulding machine will deliver stable quality, lower scrap, and more predictable output, which is exactly what you want if you’re serious about efficient, high‑volume injection moulding.
Common Problems with Injection Moulding Machine Products
Even the best injection moulding machine products can cause issues if the setup, maintenance, or process control isn’t right. I’ll keep this straight and practical so you can link machine behavior to part quality fast.
Typical Defects Linked to Machine Issues
Most quality problems come back to the machine, not just the mold or material. Common defects tied to plastic injection equipment include:
- Short shots – often caused by low injection pressure, undersized injection unit, worn non-return valve, or air leaks.
- Flash – usually from insufficient clamping force, poor platen parallelism, or worn tie bars and bushings.
- Burn marks – linked to trapped air from low venting combined with too high injection speed or heater overshoot.
- Sink marks / voids – low packing pressure, too short holding time, or a machine that can’t maintain consistent pressure.
If you’re fighting recurring defects, it’s worth reviewing the full list of injection moulding defects and root causes in this practical defect troubleshooting guide.
Troubleshooting Inconsistent Shot Size and Pressure
Inconsistent shot size and pressure are classic injection moulding machine product problems:
- Check screw check-ring / non-return valve wear – if it’s leaking, your shot will vary.
- Verify back pressure, screw recovery time, and cushion – these must be stable cycle to cycle.
- Confirm material feed – blocked hopper, wet material, or bridging will hit shot repeatability.
- Monitor the hydraulic or servo-hydraulic system – unstable pump output gives unstable pressure.
- On all electric injection molding machines, check motor tuning and pressure calibration.
If the machine can’t hold a stable cushion and pressure, no process setting will save part consistency.
Handling Flash, Short Shots, and Burn Marks
You’ll see these across all injection molding machine types (hydraulic, all-electric, hybrid). Basic direction:
- Flash
- Increase clamping force or move to a higher-tonnage plastic injection moulding machine.
- Reduce injection pressure and speed.
- Check mold parting line, platens, and tie bars for wear or misalignment.
- Short shots
- Raise melt temperature, injection speed, and injection pressure.
- Increase shot size and holding pressure / time.
- Confirm venting and gate size – if those are OK, look at the injection unit specifications (shot size and pressure capacity).
- Burn marks
- Reduce injection speed and melt temperature.
- Improve venting and check gate design; this is where a solid gate design approach like in this gate in injection moulding overview really helps.
- Check barrel heaters and thermocouples for overshooting.
Adjust Process vs Service the Machine
You don’t always need a technician; sometimes you just need smarter process changes. A quick rule:
- Adjust the process when:
- Part issue appeared after a mold change, material change, or setting change.
- Machine parameters are stable and repeatable.
- You can see clear process knobs: temps, speeds, back pressure, pack/hold, cooling.
- Service the machine when:
- Problems persist across different molds and materials.
- You see drifting temperatures, drifting injection pressure, or unstable cushion.
- There are leaks, abnormal noises, vibration, or slow/clunky movements.
- Energy use spikes or the automatic injection moulding machine alarms frequently on pressure/position.
If you’re constantly “tuning” a process that was once stable, the machine likely needs service, not more tweaking.
How Poor Maintenance Kills Quality and Drives Scrap
Skipping preventive maintenance on injection moulding machines is expensive:
- Worn screw/barrel and check ring = inconsistent melt and shot size → higher scrap.
- Dirty filters and old hydraulic oil = unstable pressure and temperature → random defects.
- Miscalibrated sensors and heaters = melt degradation, burn marks, warpage.
- Loose platens and worn tie bars = flash and dimension drift.
- Poor lubrication = jerky clamp movement, slower cycles, higher energy use.
If your scrap rate is climbing and nothing “obvious” changed in the mold or material, the machine and its maintenance history should be the first place you look.
FAQs on Injection Moulding Machine Products
Hydraulic vs electric injection moulding machine products
Hydraulic injection moulding machines are tough, proven, and handle high-tonnage, thick-wall, and general-purpose parts at a lower upfront price. They’re the workhorse in many automotive and heavy-industry applications.
All-electric injection moulding machines are faster, quieter, cleaner, and extremely precise, making them ideal for medical, electronics, thin-wall packaging, and high-cavitation molds. They offer better repeatability and lower energy use but cost more upfront.
Hybrid injection moulding machine products sit in the middle: electric where precision and speed matter (screw, dosing, clamp) and hydraulic where raw force is needed.
Typical cost range of injection moulding machine products
Prices vary by tonnage, brand, and configuration:
- Small injection moulding machines (≤100T): roughly $15,000–$60,000
- Medium (100–350T): roughly $40,000–$150,000
- Large tonnage machines (400T+): can go from $120,000 into the high six figures
Options like multi-shot, vertical clamp, high-speed packaging specs, or Industry 4.0 control will push the price up. Always factor in tooling, auxiliaries, and automation when budgeting.
How to estimate tonnage for a specific part
You don’t need an exact formula to get a good estimate:
- Calculate projected area of the part + runner (cm² or in²).
- Multiply by cavity count.
- Use a pressure factor:
- General parts: ~3–4 tons per in² (45–60 kN per cm²)
- Thin-wall or high-pressure resins: 4–6+ tons per in²
Then add a safety margin of 10–20%. If you’re outsourcing the molding, you can share your 3D model with a professional plastic injection moulding company and they’ll confirm the clamping force for you.
Using recycled plastic materials in injection moulding machines
Modern plastic injection equipment can run recycled materials, but you need to control:
- Material quality: clean, sorted, and consistent regrind
- Drying: recycled materials often absorb more moisture
- Screw and barrel wear: abrasives and fillers in recycled resin can increase wear
- Process windows: expect narrower windows and more tuning on temperature and back pressure
For many projects, a blend of virgin + recycled resin gives a safer balance of performance, cost, and sustainability. This is common in automotive and packaging plastic part manufacturing.
Energy efficiency expectations of modern machines
Energy-efficient molding machines are standard now, especially servo-hydraulic and all-electric designs:
- Energy savings: ~30–70% vs old fully hydraulic machines
- Servo drives: only consume power when movement is needed
- Better insulation and efficient heaters cut barrel energy use
- Smart control systems optimize pump and motor load
When comparing machines, look at kWh/kg for your target parts, not just the marketing numbers. Over a few years, energy efficiency often outweighs the price difference.
Lead time and installation for a new injection moulding machine product
Typical timelines we see in the global market:
- Lead time: 6–14 weeks for standard models; longer for custom, multi-shot, or large tonnage machines
- Shipping + customs: add 1–4 weeks depending on your region
- On-site installation: usually 2–5 days to position, level, connect power, water, and peripherals
- Commissioning & training: 1–2 weeks for process setup, trial runs, and operator training
Plan your machine purchase together with mold build, auxiliaries (chiller, dryer, compressor), and material selection. If you also need a partner for custom plastic injection moulding, align those timelines so your production can start smoothly.



 English
 French
 German
 Spanish
 Italian
 Polish
 Russian
 Japanese
 Korean
 Arabic
 Dutch
 Portuguese
 Swedish
 Norwegian
 Belarusian
 Armenian